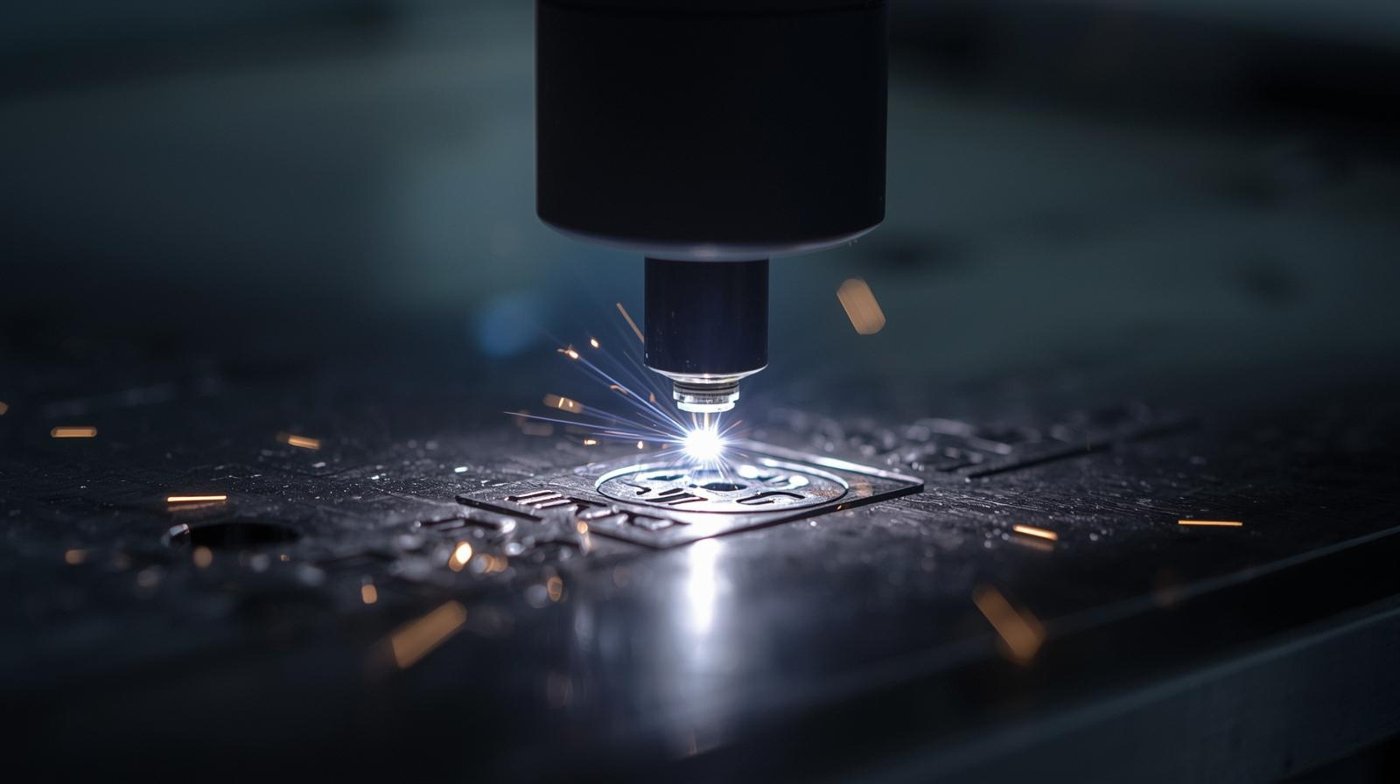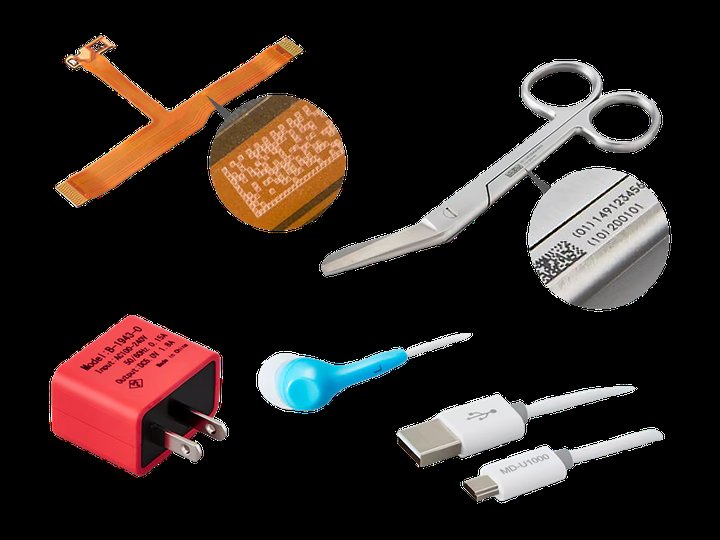
Tool makers want a part number or brand that survives heat treatment, grinding and years of abrasion. That means removing material — typically 0.1 to 1 mm — rather than changing its colour.
Power and passes
A 50 W fiber source engraves hardened steel at roughly 0.02–0.04 mm per pass at 20 kHz. A 0.5 mm deep logo of 20 × 20 mm therefore takes 15–25 passes and two to four minutes. Doubling power to 100 W roughly halves the time; MOPA sources with longer pulse widths remove material faster still.
Lens choice
Use the smallest field that fits the job. A 110 × 110 mm F-theta lens focuses to a smaller spot with higher energy density than a 200 × 200 mm lens, so it engraves deeper per pass. For dies with recessed faces, a 3D galvo keeps focus across the height difference.
Getting a clean floor
- Rotate the hatch angle by 30–45° each pass to avoid ridges.
- Use air assist to blow melt out of the groove.
- Finish with one low-power cleaning pass to remove oxide.
Our tabletop and enclosed fiber machines are the usual fit; for heavy dies we build a customised gantry with an XY stage so the part never needs lifting.